 Global Presence
Manufacturing Excellence
Our manufacturing plants are designed and built to meet the highest international standards, With 25 state-of-the-art manufacturing facilities strategically located across India, we ensure efficiency, precision, and scalability in every step of our production process.
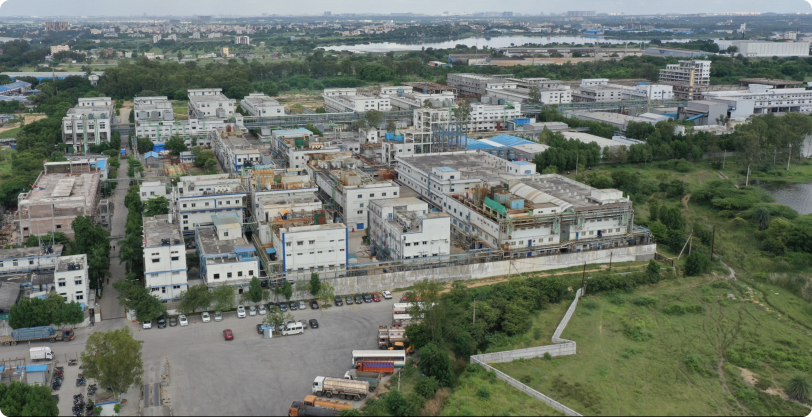
25 State of the Art Manufacturing Facilities
17
API Manufacturing Facilities
8
Formulations Manufacturing Facilities
API Manufacturing
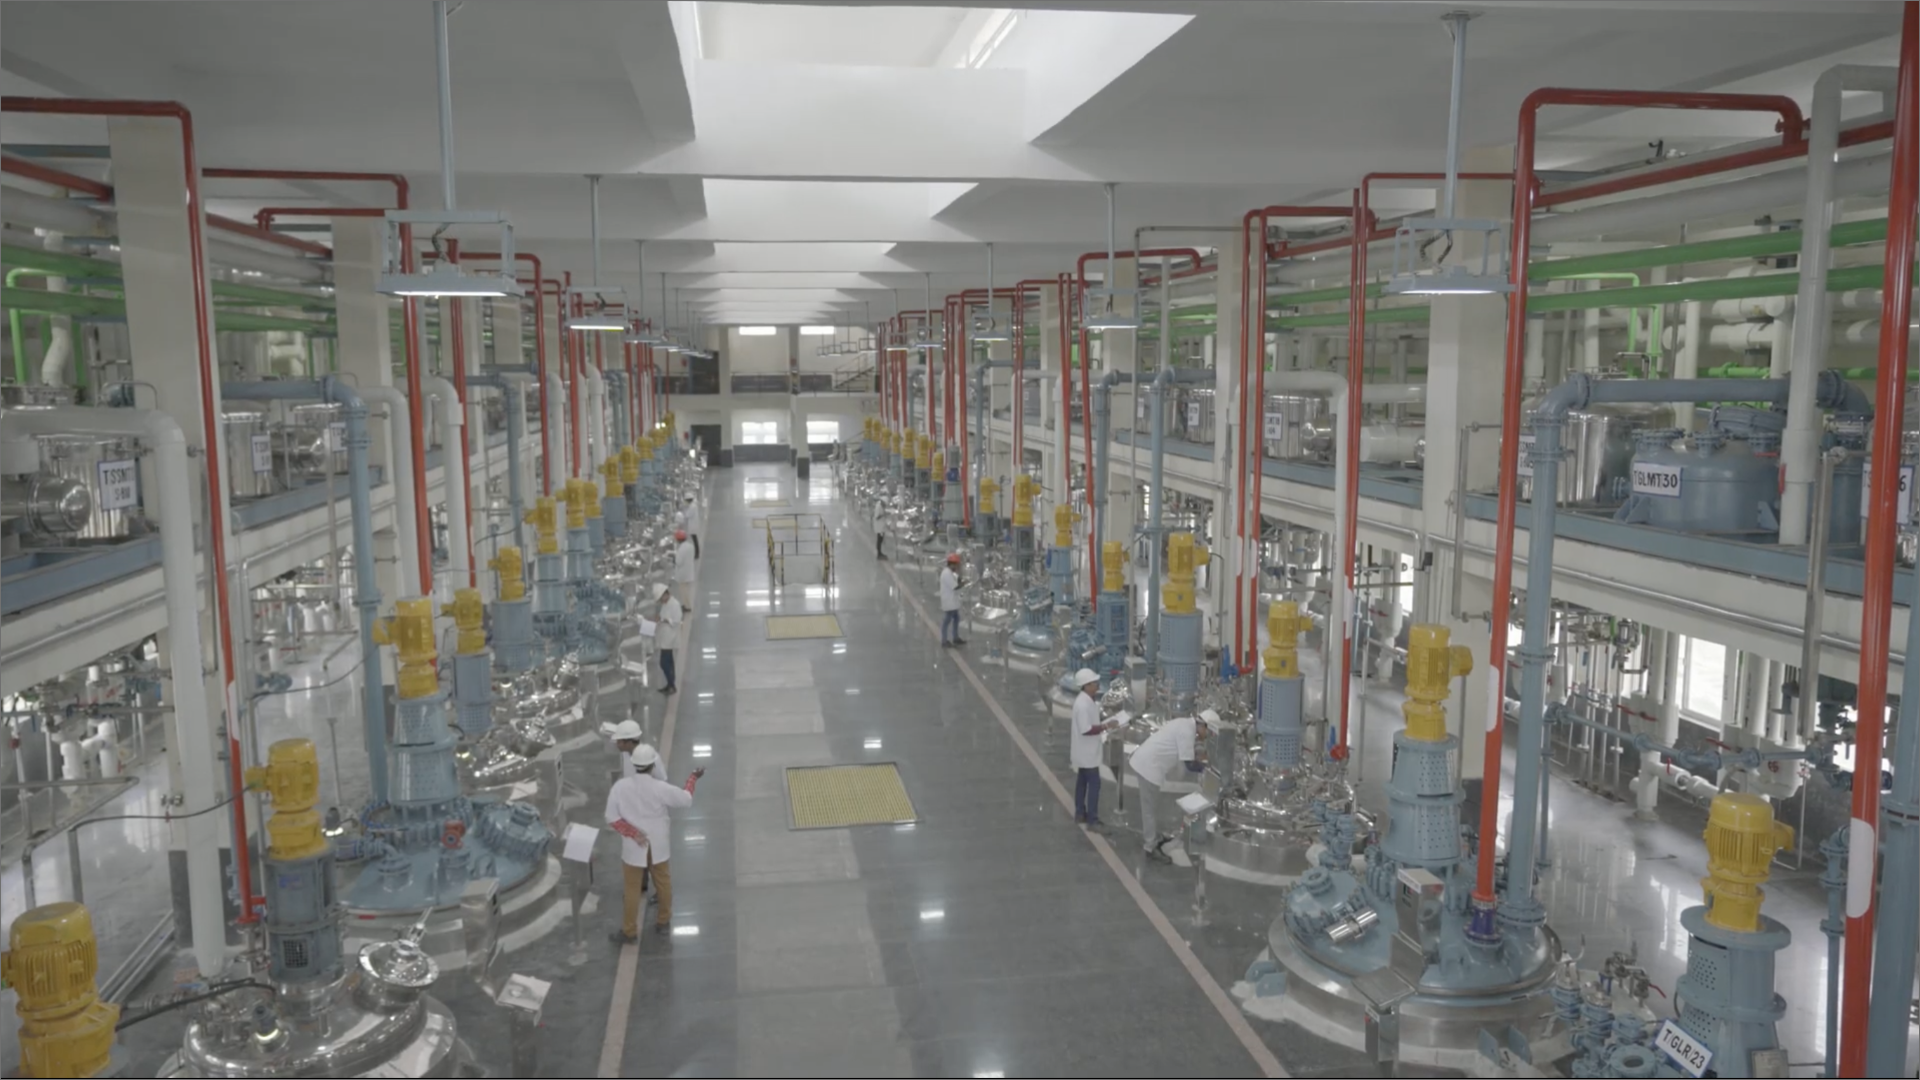
As one of the fastest-growing pharmaceutical companies in the country, MSN Laboratories has established itself as a global leader and star supplier in the API sector.
With 17 world-class API facilities, including specialized units for Cytotoxics and Prostaglandins, we are a trusted partner to businesses worldwide.
Our APIs reach over 1000+ international pharma companies as customers across more than 60+ therapeutic areas, reflecting our commitment to excellence and innovation.
At the heart of our success lies a combination of exceptional research talent, innovative development strategies, and operational efficiency. This dynamic synergy has propelled MSN Laboratories to achieve remarkable growth while consistently meeting our customers’ production requirements and delivering on time. Our relentless pursuit of excellence continues to solidify our reputation as a reliable and forward-thinking partner in the global pharmaceutical landscape.
17
API Production sites
500+
Acres of area
2400
Reactors
10000 KL
reaction volumes
2500
MT Installed API Capacities
API Accreditations
Formulations Manufacturing
MSN Laboratories has strong formulation manufacturing capabilities across a wide range of finished dosage forms, including tablets, capsules, sublingual tablets, liquids, sachets, prefilled syringes (PFS), ampoules, vials, and lyophilized vials, supporting a portfolio of over 300 products for global markets.
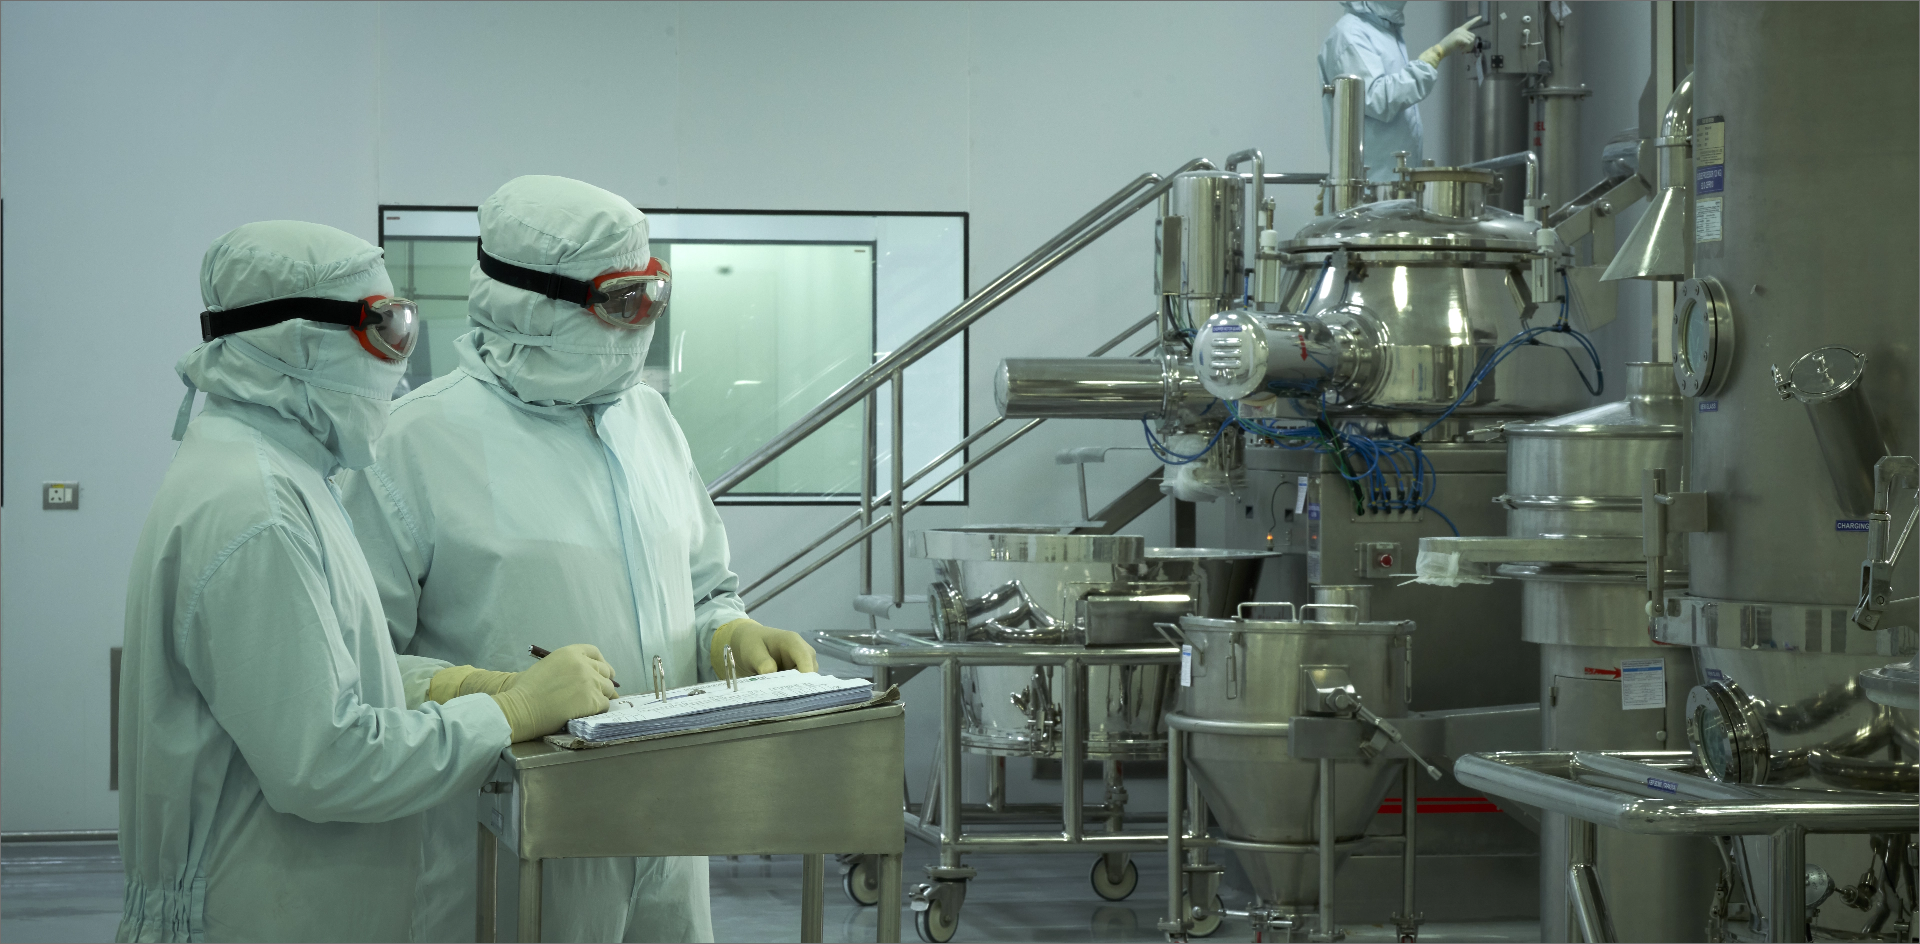
The facilities are equipped with advanced technologies such as wet and dry granulation, direct compression, film coating, and high-quality blister, strip, and alu-alu packing, along with dedicated lines for oral solids and liquid and lyophilized parenterals. All manufacturing sites operate under stringent Class 10,000 and Class 1,000 controlled conditions, supported by dedicated AHUs, terminal HEPA filtration in critical processing areas, and robust safety and compliance systems, including specialized units for general formulations, oncology, and C-II controlled products, with dedicated oncology blocks built to OEM-4 conditions to ensure quality, containment, and patient safety.
~ 15 Billion
Tablets
~ 4.0 Billion
Capsules
~120 Million
Sachets
~40 Million
Parenterals
~8.0 Million
Oral Suspensions
~3000 Tons
Granules
FDF Accreditations
Unmatched Capacity and Flexibility
Our facilities cater to diverse therapeutic categories, including oncology, cardiology, gastroenterology, diabetology, and pain management. With robust capabilities for oral solids, injectables, topicals, and novel drug delivery systems, we remain agile to meet the evolving demands of the global healthcare landscape.
Focus on Innovation
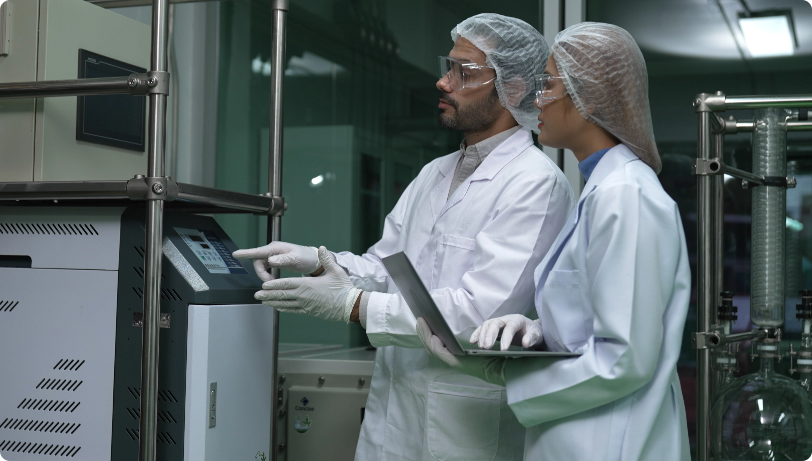
Innovation thrives across our facilities, where cutting-edge R&D integrates seamlessly with production. Our emphasis on backward integration ensures end-to-end control over the supply chain, strengthening product quality and delivery timelines.
Commitment to Sustainability
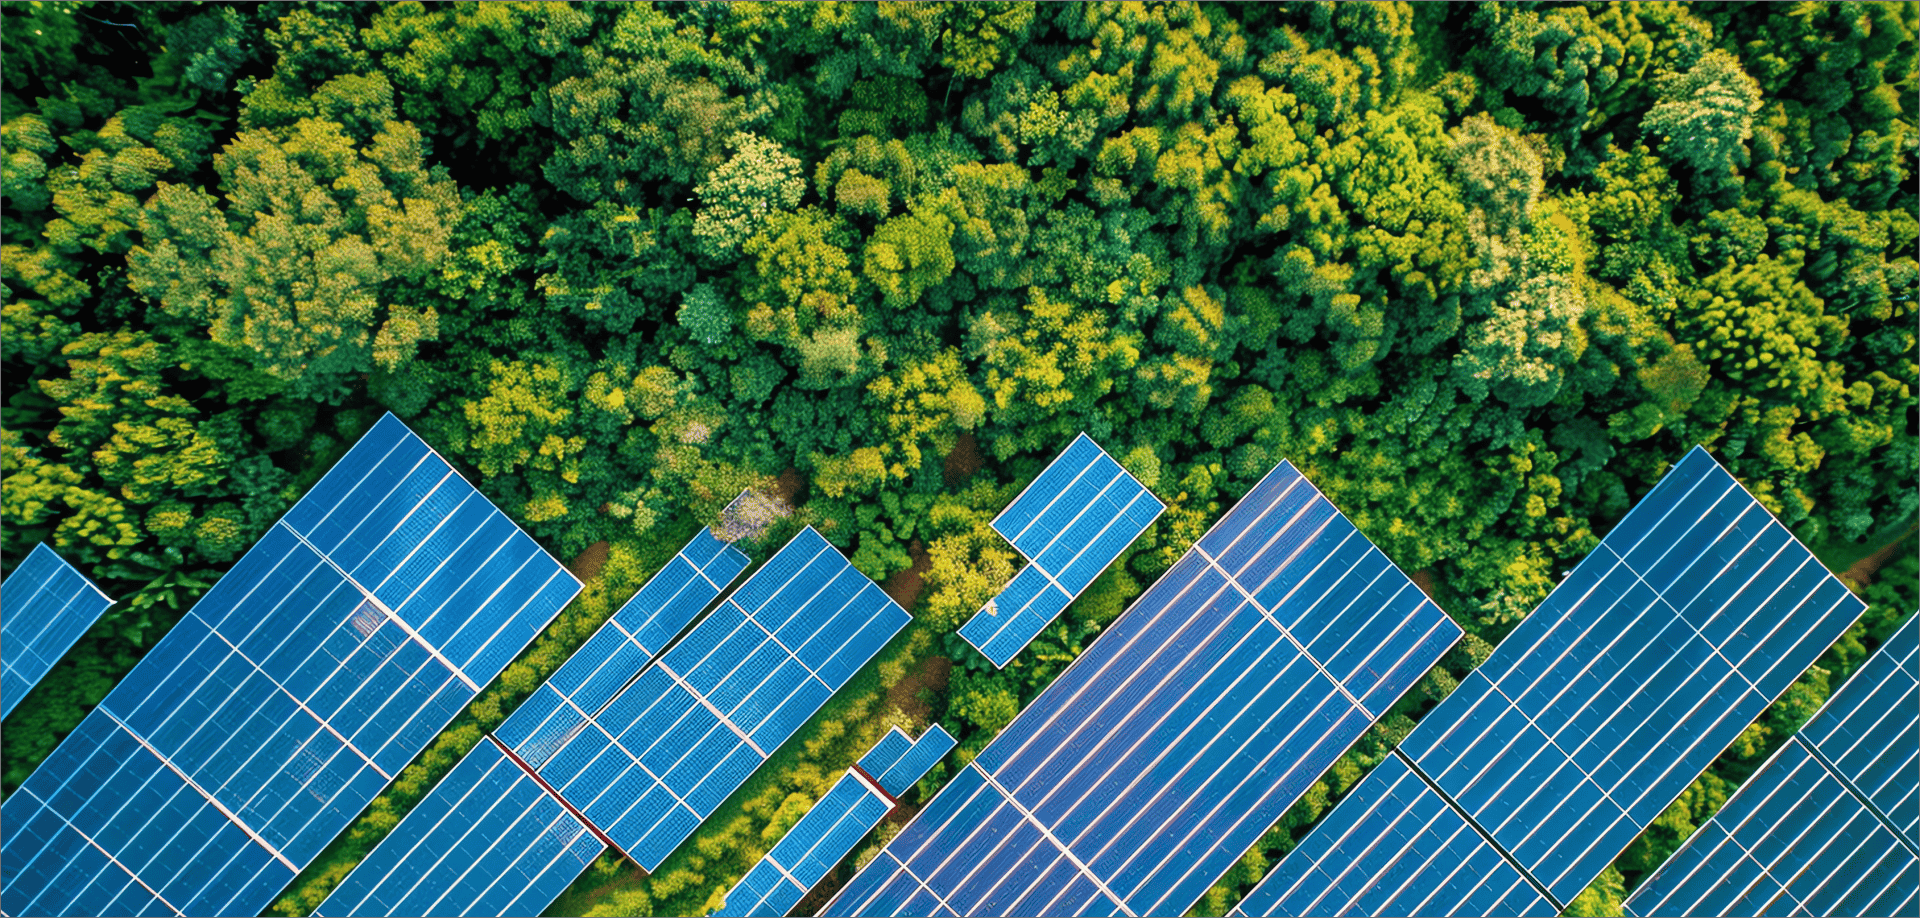
Environmental sustainability is embedded into our manufacturing ethos. By incorporating green chemistry, energy-efficient systems, and responsible waste management practices, we actively contribute to a healthier planet
- Increased renewable energy usage by 43%, significantly reducing our carbon footprint.
- 52% of our wastewater is recycled or reused, emphasizing our commitment to water conservation.
- Our advanced solvent recovery system minimizes solvent losses by 29%, showcasing efficient resource management.
- By integrating green chemistry, we drive sustainability throughout our production lifecycle, reducing environmental impact at every step.

